Extension Foundation Online Campus
Efrainbauer
Modern production centers depend on accurate chemical handling to maintain product high quality, process uniformity, and work environment safety. An Ultra high purity chemical delivery system is created to carry and dispense very detoxified chemicals while lessening contamination, leak, and direct exposure risks. These systems are specifically crucial in markets such as semiconductor manufacturing, pharmaceuticals, biotechnology, and progressed materials manufacturing. Because numerous procedure chemicals can be destructive, responsive, or harmful, safety and security must be incorporated into every stage of delivery.
Leak Detection and Containment

Among one of the most important safety functions of an Ultra high purity chemical delivery system works leakage discovery and control. Specialized sensing units can keep an eye on equipment locations for unforeseen chemical launches, while secured connections and meticulously engineered piping help in reducing the opportunity of leaks. Second control frameworks can supply an added layer of defense by collecting accidental launches before they spread throughout a facility.
Automated alarm systems can notify drivers when irregular problems are found. Early discovery allows personnel to react quickly, isolate affected sections, and lower potential damage to devices and employees.
Automated Pressure and Flow Control
Accurate pressure and circulation management is an additional essential safety and security function. An Ultra high purity chemical delivery system can include stress regulators, control valves, flow meters, and automated surveillance equipment to maintain stable operating problems. Extreme pressure might put unneeded anxiety on pipelines, fittings, and vessels, while irregular flow can affect both safety and production performance.
Modern control systems can continuously check operating parameters and initiate safety activities when analyses relocate outside predefined restrictions. Automated closure features can help avoid hazardous conditions from becoming bigger cases.
Material Compatibility and System Integrity
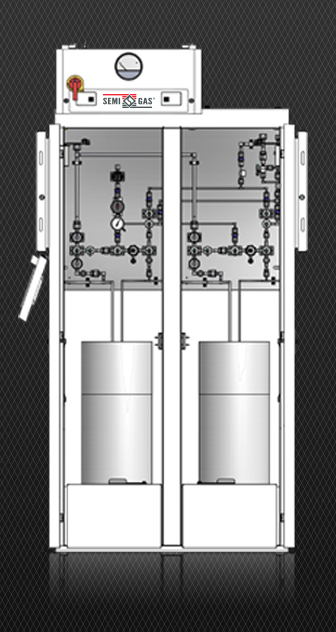
The products made use of in an Ultra high purity chemical delivery system have to work with the chemicals being transferred. Top quality tubing, valves, seals, installations, and storage components are chosen according to chemical residential properties and operating problems. Proper material choice helps reduce corrosion, destruction, particle generation, and unforeseen responses.
System integrity also depends upon proper setup and maintenance. Routine inspections can recognize worn seals, damaged elements, or potential contamination points before they come to be serious troubles. Maintaining tidy and appropriately set up links is especially vital in high-purity production settings.
Ventilation and Chemical Exposure Protection
Ventilation systems provide an additional vital layer of security. If a chemical launch takes place, properly created exhaust and air flow equipment can aid control airborne pollutants and guide them towards proper therapy or purification systems. An Ultra high purity chemical delivery system might additionally include enclosed handling areas to decrease the opportunity of direct employee exposure.
Facilities usually combine design controls with ideal operating procedures and individual protective tools. With each other, these procedures assist develop several barriers in between hazardous chemicals and employees.
Monitoring, Automation, and Emergency Situation Closures
Advanced automation has considerably improved the security of chemical shipment operations. Sensing units can keep an eye on stress, temperature level, flow, storage space degrees, and leak problems in genuine time. Control software application can evaluate these dimensions and alert drivers when uncommon problems occur.
Emergency closure systems are specifically important since they can quickly separate chemical sources or quit distribution when a dangerous problem is discovered. Depending upon facility layout, automated interlocks might stop certain procedures from proceeding unless needed safety problems are pleased. This decreases reliance on hands-on intervention throughout vital scenarios. See this web site https://www.chengweisemi.com/application/ ready to recognize extra.
Upkeep, Training, and Safe Procedure

Modern technology alone can not assure safe chemical handling. An Ultra high purity chemical delivery system requires regular maintenance, evaluation, calibration, and testing to stay reputable. Operators ought to obtain ideal training covering system operation, chemical hazards, emergency treatments, and contamination-control methods.
Clear treatments for start-up, closure, chemical replacement, upkeep, and emergency reaction can better reduce functional dangers. By integrating robust devices with experienced personnel and self-displined upkeep methods, facilities can create a much safer and even more trustworthy chemical delivery setting.
Modern safety features therefore make an Ultra high purity chemical delivery system a crucial element of sophisticated manufacturing facilities. Leak discovery, automated controls, compatible products, ventilation, tracking, emergency situation closures, and efficient training interact to secure personnel, tools, procedures, and product top quality.